
Scratch-dig surface quality describes limits on visible imperfections in an optical surface. Under the MIL-PRF-13830B convention, 40-20 means a scratch comparison grade of 40 and a maximum dig diameter of 0.20 mm; 60-40 means grade 60 and 0.40 mm. Lower numbers set tighter limits within the same inspection system. The scratch number is not a width in micrometers, and neither number specifies surface flatness or laser damage resistance.
For buyers comparing lenses, windows or prisms, the useful question is which imperfections the application can tolerate and how the finished part will be inspected. A grade becomes meaningful when it is tied to a standard, an identified surface and an inspection region.
How to Read 60-40, 40-20 and 20-10
The two numbers use different scales. A scratch is evaluated against a reference standard under prescribed viewing conditions. A dig is a localized pit or similar defect whose size is expressed in hundredths of a millimeter. Edmund Optics’ surface quality guide explains this distinction between scratch visibility and dig size.
| Specification | Scratch grade | Maximum dig diameter |
|---|---|---|
| 60-40 | 60 | 0.40 mm (400 µm) |
| 40-20 | 40 | 0.20 mm (200 µm) |
| 20-10 | 20 | 0.10 mm (100 µm) |
These are grade interpretations, not complete acceptance rules. For an irregularly shaped dig, MIL-PRF-13830B uses the average of its maximum length and maximum width to determine diameter. A scratch grade of 40 does not mean a 40 µm-wide scratch, and changing from grade 60 to 40 does not define a proportional reduction in scratch width.
One Small Defect Does Not Set the Whole Result
A surface can contain several defects below the maximum individual limit and still fail the applicable specification. Acceptance also depends on cumulative scratch lengths, dig quantity and distribution, and the region being evaluated. Sections 3.5 and 4.2.2 of MIL-PRF-13830B, reproduced by Knight Optical, set out the surface requirements and inspection methods.
Define the clear aperture or test region on the drawing. A mark outside the working optical area may be assessed differently from one inside it, but an unspecified edge area should not automatically be treated as unrestricted. Noncircular optics and separately specified zones also require the appropriate assessment rules. This matters for custom windows and shaped components whose usable optical area is smaller than their outline.
Surface Quality, Surface Figure and Roughness Answer Different Questions
A lens can meet its scratch-dig requirement while missing another optical requirement. Keep the following properties separate when comparing supplier specifications:
- Surface quality: allowable localized imperfections such as scratches and digs.
- Surface figure or flatness: deviation from the intended surface shape, evaluated over a defined area.
- Surface roughness: fine-scale surface texture, commonly described by a measured roughness parameter and its measurement conditions.
These distinctions are covered in Edmund Optics’ optical specifications reference. A 20-10 callout alone does not establish a particular flatness, roughness, transmission or wavefront result. Coating adhesion, resistance to cleaning and environmental performance also need their own requirements, as explained in our guide to optical coating durability.
Choose the Grade Around the Optical System
The same surface mark can have different consequences in different optical positions. A window in a light-collection system may tolerate imperfections that would be objectionable near an image plane or in a measurement channel sensitive to scattered light. The wavelength, illuminated area and permitted stray light all help determine how demanding the requirement should be.
Laser applications need particular care because surface defects can contribute to damage initiation. However, a tighter scratch-dig grade does not certify a laser-induced damage threshold. The coating, substrate and actual laser operating conditions still need separate evaluation. Avoid selecting a grade solely from labels such as “laser quality” or “high precision.”
Moving from 60-40 to 40-20 tightens both defect limits, but the benefit should be justified by the system’s needs. Unnecessary tightening can increase manufacturing and inspection cost without improving the result that matters to the user. For an established design, follow its approved requirement; for a new design, have the optical designer connect the proposed grade to the performance target.
Agree on Inspection Before Comparing Results
Scratch visibility changes with illumination, viewing direction and background. A phone photograph or an inspection under an arbitrary bright lamp cannot establish a MIL scratch grade. Buyer and supplier should identify the applicable method, comparison reference and inspected surfaces so that incoming inspection uses the same basis as acceptance at the supplier.
For a coated optic, state whether the requirement applies to the uncoated substrate, the finished coated component, or both. Passing an inspection before coating does not by itself establish the condition after subsequent processing and handling. Likewise, loose contamination should be distinguished from permanent surface damage using the approved inspection and cleaning procedure. Our article on clean handling of optical components discusses how surface condition can change during replacement.
Read ISO Drawing Requirements in Their Own Context
ISO 10110-7:2017 addresses acceptable surface imperfections within a test region on optical elements and assemblies. It allows requirements based on the area affected by imperfections or on their visibility. Therefore, an ISO surface-imperfection callout should be interpreted with its stated method and drawing notes; it should not be converted to a MIL scratch-dig pair by guesswork.
When two quotations use different conventions, ask for the inspection basis to be reconciled before comparing the grades. Matching the numbers while changing the method can leave a different acceptance requirement.
Applying the Requirement to an Order
For a purchase specification, connect the required grade to the named standard and revision, identified faces, clear aperture and condition after coating where applicable. Agree how inspection results will be documented. This gives the surface-quality requirement a usable meaning throughout the order.
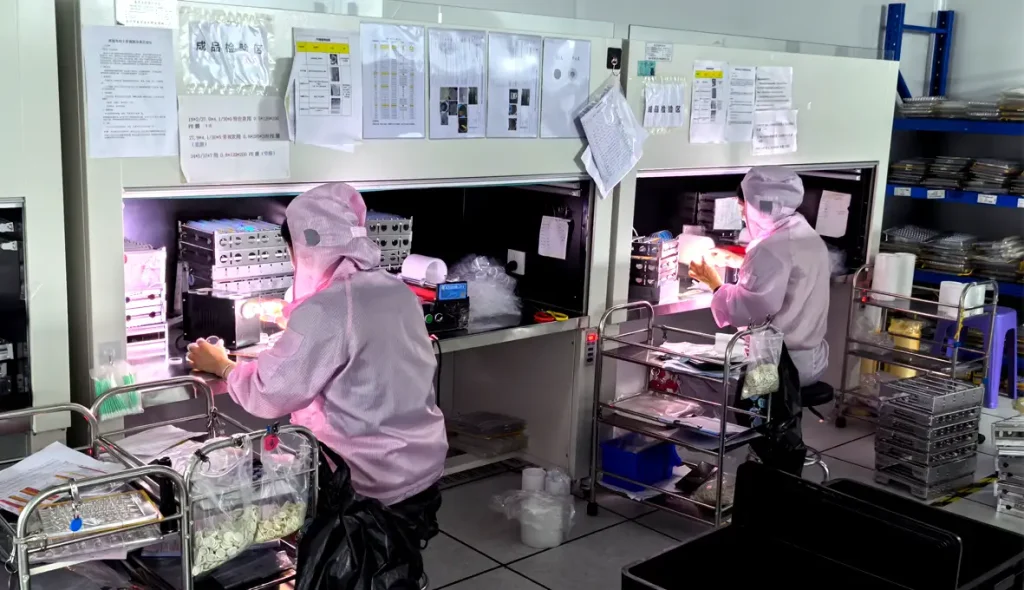
Likai Laser supplies standard and custom optical components and evaluates manufacturing and coating requirements against the intended application. The featured photograph shows optical component inspection and handling in the manufacturing environment; it does not demonstrate a particular scratch-dig grade. Any required grade and inspection scope need confirmation for the specific component.